ADC12 for automotive die casting
The working alloy for transmission housings, motor and inverter housings, oil pans and EV battery trays. Certified to EN and JIS on a single material test certificate, with CBAM emissions documentation on every shipment.
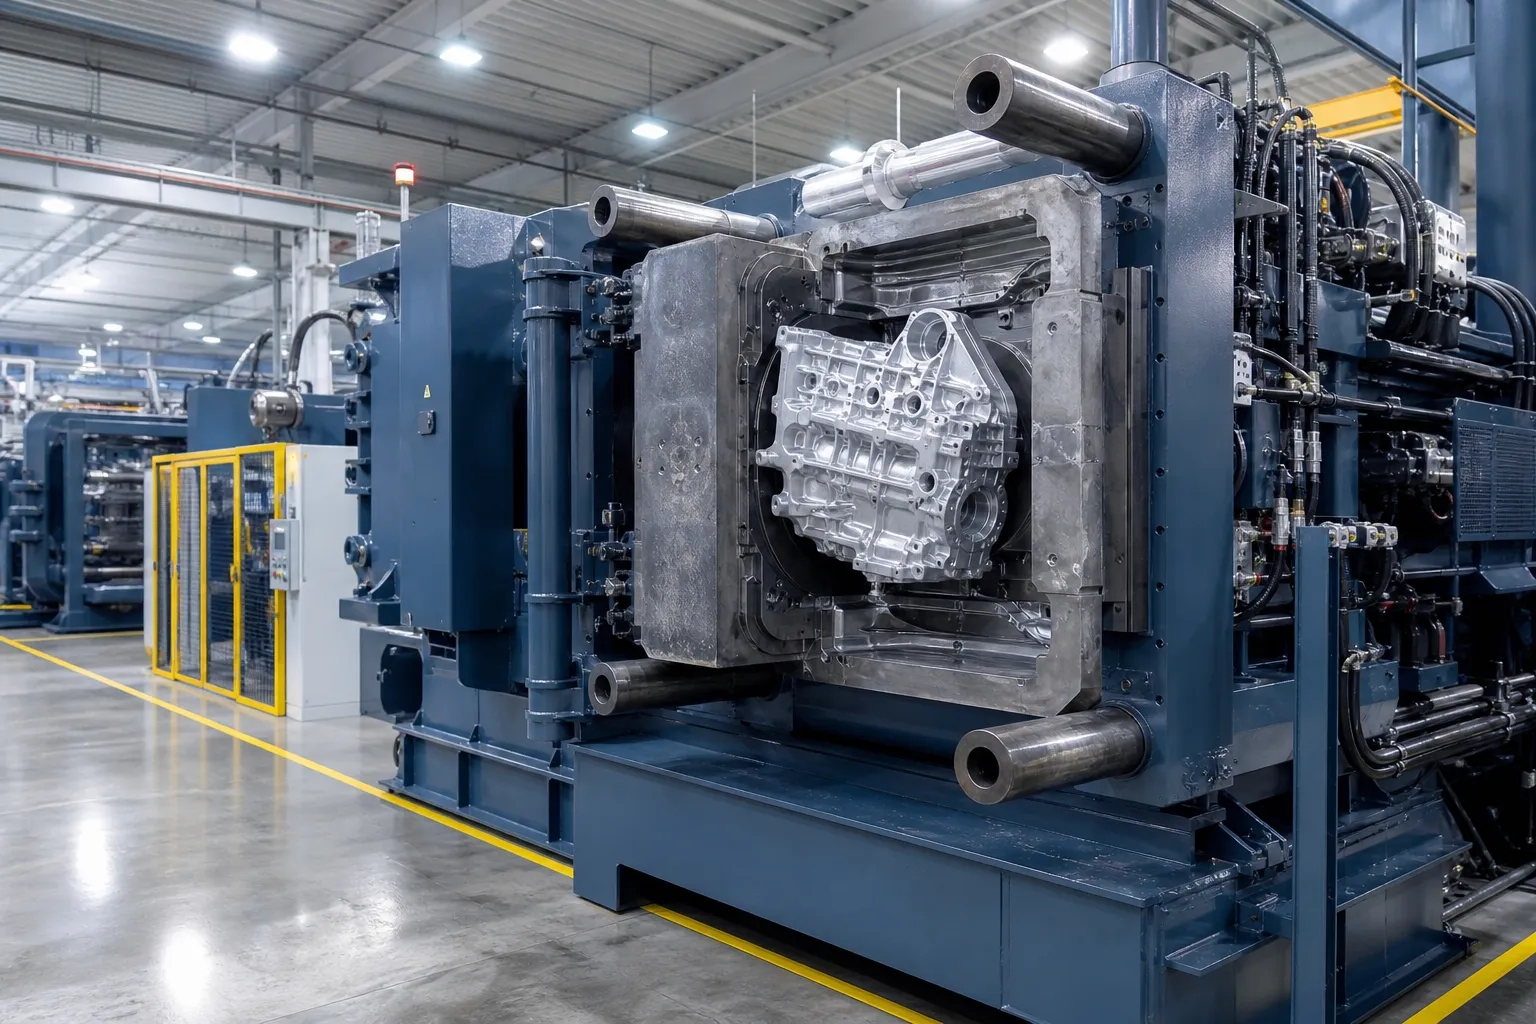
What a production die-casting line actually needs from its ingot
Automotive die casting runs at volume and at speed. The alloy has to fill a complex die in milliseconds, release cleanly, hold dimension through solidification, and behave the same way on the last shot of a heat as it did on the first. Most of that behaviour is determined before the metal reaches your furnace, by the chemistry of the ingot you bought.
Which alloy belongs in which component
ADC12 is the right answer for most automotive die castings, and the wrong answer for a few of them. We would rather quote you the correct alloy than the one we have most of.
| Component | Alloy | Why |
|---|---|---|
| Transmission and gearbox housings | ADC12 | Pressure tightness and dimensional stability across thin, cored sections |
| Motor, inverter and e-drive housings | ADC12 | Complex cores, good thermal path, stable as-cast properties |
| Oil pans, timing covers, bell housings | ADC12 | Fluidity to fill large thin sections in a single shot |
| EV battery trays and covers, non-structural | ADC12 | Large thin-wall castings at volume, no load-bearing duty |
| Engine blocks and bedplates | ADC12 | Silicon for wear resistance, copper for strength at temperature |
| Cylinder heads | AL-Si (AlSi7Mg / AlSi10Mg) | Heat treatable, holds fatigue strength at operating temperature |
| Structural nodes and crash elements | AL-Si (low-iron AlSi10MnMg) | Needs 8 to 12% elongation and weldability that ADC12 cannot reach |
| Cast road wheels | AL-Si (AlSi7Mg) | Ductility and fatigue life for a safety-critical rotating part |
Casting a structural part? See our AL-Si alloy range, or send the drawing and we will tell you which specification fits.
What changes when you buy direct from the smelter
Frequently asked questions
Which aluminium alloy should I use for EV battery enclosures?
It depends on whether the enclosure carries structural load. Non-structural trays, covers and housings are routinely cast in ADC12, which fills large thin-walled sections reliably at high volume. Enclosures that form part of the crash structure need far higher ductility than ADC12 provides, and are normally cast in a low-iron AlSi10MnMg or AlSi7Mg alloy. Tell us which case applies and we will quote the correct alloy rather than the convenient one.
Can ADC12 be used for structural or crash-relevant castings?
Generally no. ADC12 contains 1.5 to 3.5% copper and up to 1.3% iron, which give it strength, machinability and excellent die-casting behaviour, but leave elongation typically in the 1 to 3% range. Structural and crash-relevant castings need 8 to 12% elongation and the ability to be riveted or welded into a body-in-white. Those parts call for a low-iron AlSi10MnMg type alloy. ADC12 remains the right choice for housings, covers and enclosures that are not load-bearing.
What iron content do you supply for high-pressure die casting?
Our standard ADC12 runs iron in the 0.8 to 1.1% band. That is deliberate. Below roughly 0.7% iron, aluminium tends to solder to steel dies in high-pressure die casting, shortening die life and causing surface defects. Above about 1.2%, brittle beta-AlFeSi platelets form and reduce ductility. If your process window needs a different iron target, specify it on the enquiry and we will cast to it.
Can you certify ADC12 to A383 limits for a North American customer?
Yes. ADC12 overlaps most closely with ASTM A383, which carries tighter iron and zinc limits than the base EN AC-46000 specification. If your downstream customer requires A383 compliance, note it on your enquiry and we will tighten the heat composition and certify accordingly on the material test certificate, at no additional cost on standard-tonnage orders.
Do you provide CBAM emissions data for automotive castings entering the EU?
Yes. Every shipment carries verified embedded-emissions data covering direct and indirect emissions per tonne of finished ingot, calculated to the EU CBAM methodology and verified by an accredited third party. Egypt's hydroelectric base at Aswan typically produces lower embedded emissions than aluminium from coal-grid jurisdictions, which means fewer CBAM certificates against your import. Read the full CBAM guide.
Can we run a trial melt before switching supplier?
Yes, and we expect it. First-time European buyers can order 5 to 10 tonnes for qualification testing rather than a full 20 tonne container. Most foundries run the trial alongside their incumbent supply for one or two production weeks, checking die fill, soldering behaviour and machined surface finish before committing to a contract volume.
Send us the part, we will tell you the alloy
Give us the component, the annual volume and the delivery port. Noel Murphy replies within 24 hours with pricing, lead time and CBAM documentation.